Machine vision uses the latest artificial intelligence technology to enable industrial equipment to observe and analyze tasks in smart manufacturing, quality control and labor safety, thereby improving product quality, reducing costs and optimizing operations.
What is Machine Vision?
Simply put, machine vision technology gives industrial equipment the ability to "see" what it's doing and make quick decisions based on what it sees. The most common uses of machine vision are visual inspection and defect detection, locating and measuring parts, and identifying, sorting and tracking products.
Machine vision is one of the basic technologies of industrial automation. It has been helping improve product quality, speed up production and optimize manufacturing and logistics for decades. Now, this proven technology is merging with artificial intelligence and leading the transformation towards Industry 4.0.
The Origins of Machine Vision: Traditional Machine Vision Systems
Long before the advent of artificial intelligence and machine learning, machines had the ability to "see". In the early 1970s, computers began to use specific algorithms to process images and identify basic features. This traditional machine vision technique detects object edges to locate parts, finds defective color variations, and distinguishes blobs of connected pixels with holes.
The operation of traditional machine vision is relatively simple and does not require artificial intelligence. Text must be as concise and legible as a barcode. Shapes must be predictable and conform to exact styles. Traditional machine vision systems can't read handwriting, read wrinkled labels, or tell apples from oranges.
Nonetheless, traditional machine vision has had a huge impact on manufacturing. Because machines don't get tired, they can spot defects faster and more reliably than the human eye. In addition, machines are not limited by human vision. Dedicated machine vision cameras use thermal imaging to detect heat anomalies, and X-rays to find microscopic defects and metal fatigue.
The Rise of Artificial Intelligence: Deep Learning Inference and Industrial Machine Vision
Increasingly powerful edge computing (the edge of the network and other embedded and IoT devices), coupled with a growing number of artificial intelligence (AI) deep learning models, is greatly expanding the capabilities of machine vision. Rapidly growing capabilities are leading the transformation towards smart factories and Industry 4.0.
AI augments traditional computer vision algorithms through models called neural networks. When a computer receives an image or a video stream of images, machine vision software compares the image data to the neural network model. This process, known as deep learning inference, allows computers to identify extremely subtle differences, such as tiny incongruous patterns in fabrics and microscopic defects in circuit boards.
In order to improve accuracy and speed, data scientists build specific neural network models for specific applications. In a process called supervised training, the computer looks at thousands of examples and looks for meaningful patterns, including ones that humans might not detect.
Some models can detect dead and discolored pixels in displays, look for voids in solder joints, and pinpoint loose threads on fabrics. Of course, more models will be continuously developed and improved.
Smart Machine Vision and Autonomous Systems
AI is extending machine vision beyond visual inspection and quality control. Through machine vision, robots can sense in three dimensions, hold each other's parts, and check each other's work. They can even interact with their human colleagues and make sure they work together safely.
Machines with intelligent vision can use natural language processing to read labels and interpret signs. Robots with machine vision can understand shape, calculate volume, and perfectly pack boxes, load trucks, and even shipping containers without wasting space.
Moving from machines that can automate simple tasks to autonomous machines that can go beyond what the human eye sees and thinks, taking longer to optimize each component, will push industrial innovation to a whole new level.
It sounds like science fiction, but today, intelligent machine vision is at work in factories, warehouses and shipping centers, assisting and assisting workers by handling everyday tasks, allowing them to use their expertise and focus on what matters most.
Machine Vision Application
Industrial machine vision is the foundation of smart manufacturing, logistics and operations. Machine vision cameras, embedded IoT sensors, and industrial computers can bring intelligence, analysis, and efficiency to every step of the manufacturing process.
Advantages of Machine Vision in Operations
Improving worker health and safety is a key benefit of applying machine vision to operations. Computers powered by artificial intelligence ensure workers maintain social distancing and wear proper safety equipment. Robots and equipment with machine vision can understand and interact with humans to help prevent accidents before they happen. They can warn operators or automatically shut down equipment if conditions are unsafe, reducing risk to employees and your business.
In addition, by continuously analyzing data from cameras, microphones and sensors embedded in industrial equipment and machines, industrial computers can use artificial intelligence to detect failures and signs of wear and tear before failures occur, thereby enabling preventive maintenance to be planned in advance, This in turn eliminates unplanned downtime and spreads maintenance costs over time.
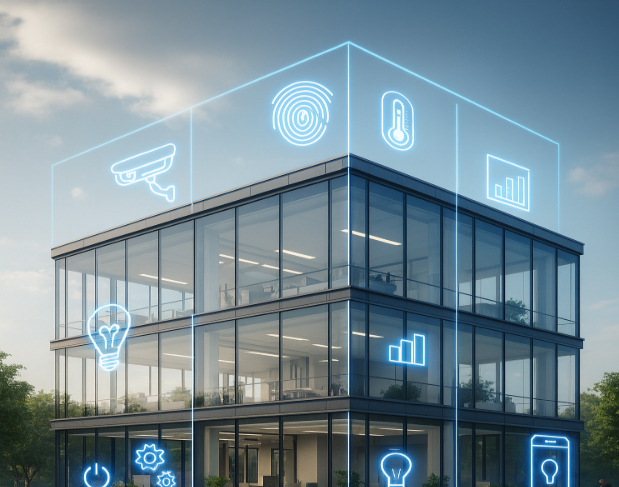
In asset management and security, AI can detect and track video sources to ensure proper use and storage, and alert management if assets move outside predefined boundaries. Security camera systems can be active security partners, controlling building access and identifying dangerous situations.
Machine vision and industrial automation provide immediate results in increased productivity, tighter quality control and higher efficiency. A cornerstone of Industry 4.0 technology, machine vision is transforming manufacturing, logistics and operations.