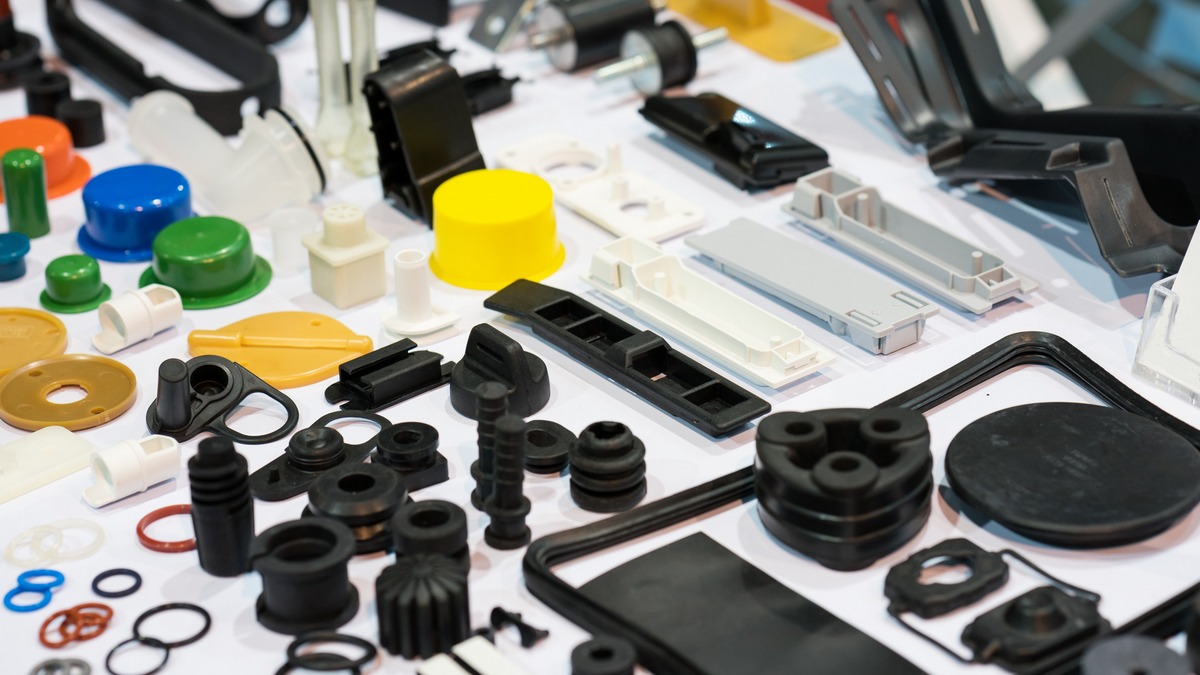
Plastic granulation technology is mainly used in plastic product manufacturing and resource recycling to make various plastic products or plastic raw materials, and has both environmental and economic benefits.
What Is the Plastic Granulation?
Plastic granulation is the process of taking plastic and size reducing it so that it can be used in to plastic manufacture. The manufacturing capabilities of injection mold machines in the plastics industry is limited. During injection, plastic product can form cooling spots and skinning. The injection system may not have an exhaust device which can lead to bubbles and radial flow patterns in the products. One solution which can just make up for the shortcomings of the injection molding machine is a twin-screw extruder used in granulation, which has a strong plasticizing ability and has an exhaust device. After the material is plasticized by the twin-screw extruder, the material can reach molecular level dispersion, and the vacuum exhaust device can draw away the excess water and impure gasses caused by decomposing material.
What Is the Extrusion Granulation?
The extrusion granulation process generally has two granulation methods, hot cutting, and cold cutting. Which granulation method is used depends on the properties of the material. Polyethylene and polypropylene generally use cold cutting, and PVC generally uses hot cutting. With the cold cutting method, the material is plasticized by the extruder and extruded into a round strip. The round extruded material is drawn to the pelletizer and cut into cylindrical particles after water cooling. The hot cutting method is to directly cut the newly extruded round plastic into pellets by attaching a rotating blade to the die plate. PVC granulation for injection molding is suitable for granulation by the hot-cutting method.
The hot-cutting granulation is mainly composed of a twin-screw extruder, die head, pelletizing device, pellet conveying device, and cooling fan. The kneaded material is sheared and plasticized by a twin-screw extruder, and then extruded to the desired shape through a fixed-shape die. The extruded material is cut into a fixed shape by a pelletizing device and is cooled by a fan during the conveying process to complete the pelletizing process.
Crushing Granulation Technology
Crushing and granulation technology involves collecting waste plastics and using crushing, cleaning, drying, pelletizing, and other procedures to recycle them. The most important step is the sorting step. With magnetic separation equipment, metal-containing impurities can be removed, and mixed plastic waste can be further sorted. Various types of single plastic recycled materials can be divided into two types; simple plastic, and composite plastic, according to the recycled plastic components.
Application of Twin-Screw Extruder Granulator
Twin-screw extruders are widely used for physical modification of polymers: blending, filling, and fiber reinforcement batching or mixing, and can also be used for extrusion of molded products. In addition, the twin-screw extruder has good feeding characteristics and is suitable for powder processing. It has better mixing, exhaust, reaction, and self-cleaning functions than the single-screw extruder, and it can process plastics and blends with poor thermal stability. The material time shows its superiority.
-
Production of Masterbatch
The mixture of plastic particles with a high proportion of additives is the masterbatch. Additives include pigments, fillers, and functional additives. They are usually powdery and easy to agglomerate. The twin-screw extruder is the key equipment of the masterbatch production line, used for the homogenization, dispersion, and mixing of additives in the polymer matrix.
-
Blending Modification
Reinforcing materials provide the best performance between the matrix and additives, fillers, and reinforcing materials. Glass fiber is the most important reinforcing material, but other fibers can also be combined with polymer-carriers. By adding fibers and combining them with polymers, a material with high strength and high impact resistance can be obtained.
-
Exhaust
Due to the mutual meshing of the two screws, the shearing process of the material at the meshing position continuously updates the surface layer of the material. This improves the exhaust effect, giving the twin-screw extruder better performance than the exhausted single-screw extruder. Exhaust performance. A threaded conveying element with a large lead is used in the exhaust section. A ring dam or reverse threaded element is usually used to build pressure in the first metering section. The melt that has passed the ring dam enters the exhaust section, the pressure is released, and the volatiles can escape.
-
Reactive Extrusion
Reactive extrusion is a special process in which monomers are bonded during the extrusion process. The twin-screw extruder is very suitable for reactive extrusion due to its excellent mixing performance. The liquid raw materials are added to the twin-screw extruder according to a determined proportion. The polymerization reaction occurs under the action of mixing and meshing, and the excess reaction heat is dissipated through the barrel. At the outlet, a gear pump is usually used to directly input the product into the water ring granulator for granulation.
-
Direct Extrusion
As the requirements for product dimensional uniformity are not high for granular extruded plastics, about 95% of granular products use twin-screw extruders for final mixing, devolatilization, and reactive extrusion. Through the use of specific heads and appropriate downstream equipment, finished products such as films, plates, pipes, and so on, can be produced in a more efficient manner. Direct extrusion can omit the steps of cooling, pelletizing, reheating, and melting, as the material is subjected to less thermal and shear stress. The entire process can save energy, and the formula can be easily adjusted. It has been used in the production of PE, TPE/TPO/TPV, PVB, wood fiber composites, foamed products, nylon, and biodegradable plastics. A gear pump is usually added to reduce pressure fluctuations in the materials and provide stable pressure for the machine head.
In the process of manufacturing each twin-screw extruder, we are committed to meeting high standard performance requirements. Each extruder undergoes strict quality control in the manufacturing process. The equipment and all components have been strictly audited and fully inspected. From design, procurement to production, we pay attention to every detail.