How chip flow, setup reduction, multi-sided machining, and automation determine whether a horizontal five-axis platform delivers practical value.
Five-axis machining is often discussed as a solution for complex geometry, but axis count alone does not determine whether a machine layout is appropriate. For many shops, the more useful question is whether a horizontal five-axis machining center can improve the complete production process—not simply the cutting path.
That distinction matters because horizontal five-axis machines combine two ideas: multi-axis tool access and a work zone arranged around a horizontal spindle. The first can reduce setups and reach angled or multi-sided features; the second can improve chip flow and support pallet-based automation. These benefits can be substantial, but only when they address real constraints in the part mix.
Why the Horizontal Layout Changes the Process
In a vertical machining center, the spindle points downward and the workpiece typically sits on a horizontal table. A horizontal machining center rotates that relationship: the spindle approaches from the side, and the workpiece is usually mounted vertically or on a rotary table.
The practical consequence is that gravity can help chips fall away from the cutting zone rather than collect on upward-facing surfaces. Okuma identifies improved chip flow as an advantage of horizontal machining, while Makino describes the upright workpiece orientation of a five-axis HMC as having chip-shedding capability. This does not eliminate the need for effective coolant delivery, washdown, or a properly sized conveyor, but it can reduce chip recutting or packing in cavities.
Chip evacuation is more than housekeeping. Sandvik Coromant notes that effective chip control and evacuation can reduce the risk of tool or workpiece damage where clearance is limited. In deep pockets, slots, and high-volume material-removal operations, machine orientation can therefore contribute to process stability.
Multi-Face Access: The Other Half of the Case
Five-axis machining adds two rotary degrees of freedom to the three linear axes. Depending on the machine and program, those axes may be used for 3+2 positional machining, simultaneous five-axis motion, or both. Autodesk notes that multi-axis machining can reduce setups and allow shorter, more rigid tools because the tool can be oriented more favorably to the workpiece.
The horizontal layout complements this capability when a component has significant machining on several sides. A rotary table can present different faces to the spindle without repeated manual reclamping. This is useful for prismatic parts with cross-holes, angled bores, pockets on several faces, or features whose positional relationships are important.
Every refixture introduces another opportunity for locating error, contamination at datum surfaces, or operator inconsistency. Consolidating operations can also reduce work-in-process movement between machines.
Horizontal Five-Axis vs. Vertical Five-Axis
| Decision Factor |
Horizontal 5-Axis |
Vertical 5-Axis |
| Chip behavior |
Gravity often helps chips fall away |
Chips may collect in pockets or on top-facing surfaces |
| Multi-side work |
Often strong with rotary/pallet workflows |
Strong, but access depends on table/trunnion geometry |
| Operator access |
Can be less direct |
Often straightforward for setup and inspection |
| Automation |
Commonly suited to pallet pools and FMS |
Also automatable; architecture varies |
| Floor space/capital |
Often higher |
Often lower for a similar work envelope |
| Best fit |
Repetitive multi-face, chip-heavy, unattended work |
General complex work, prototypes, mixed low-volume jobs |
The comparison is not a ranking. A vertical five-axis machine may be better for mold work, one-off parts, prototypes, or jobs where operator access and floor-space efficiency matter more than palletized production. The horizontal case becomes stronger when several benefits overlap.
When Does the Horizontal Five-Axis Layout Pay Off?
The first strong use case is chip-intensive machining. Aluminum structures, castings, and parts with deep cavities can generate large chip volumes. If chips repeatedly interfere with cutting, require frequent washdown, or increase recutting risk, horizontal orientation may have direct operational value.
The second is multi-face machining where datum continuity matters. If a part currently moves through several fixtures or machines, a five-axis horizontal platform may consolidate those operations. The benefit is not only shorter setup time; it can also simplify process planning by keeping more features tied to one clamping reference.
The third is automation. Horizontal machining centers are frequently designed around pallet changers, pallet pools, and flexible manufacturing systems. Okuma and Makino describe pallet-based systems that let operators prepare future work while the spindle is cutting. For repeat part families, this architecture can increase unattended hours and reduce time spent loading, indicating, and refixturing.
Where the Layout May Be Harder to Justify
A horizontal five-axis machine is not inherently the most economical answer. Higher acquisition cost, more complex workholding, larger footprint, CAM requirements, and collision-management demands all matter. Autodesk identifies programming complexity, collision risk, and skilled-operator requirements among the challenges of five-axis machining.
If most parts need machining from only one or two directions, the rotary capability may be underused. A low-volume job shop may also struggle to recover the investment unless setup consolidation creates a meaningful advantage. The evaluation should therefore compare total process cost—setup labor, handling, scrap risk, inspection, spindle utilization, and automation potential—not purchase price alone.
FAQ
1. Is horizontal five-axis machining always better for chip evacuation?
No. The orientation often gives gravity more opportunity to remove chips, but coolant strategy, tool geometry, cavity shape, material, and conveyor capacity still matter.
2. Does five-axis machining mean all five axes move simultaneously?
Not necessarily. Many jobs use 3+2 positional machining, where rotary axes orient the part and then remain fixed during a three-axis cut.
3. What parts benefit most from horizontal five-axis machining?
Parts with machining on several faces, angled features, deep cavities, high chip volumes, or repeat production requirements are common candidates.
4. Can a horizontal five-axis machine reduce fixtures?
Often, yes. Better access to multiple faces can reduce separate setups, although fixture count still depends on geometry, clamping, tool reach, and inspection needs.
5. Is an HMC automatically better for lights-out manufacturing?
No, but many HMC platforms are designed around pallet handling. Reliable unattended production still requires stable workholding, tool-life management, chip control, probing, and monitoring.
6. What should a shop measure before choosing this layout?
Useful metrics include setup hours per batch, number of re-clamps, spindle utilization, chip-related stoppages, work-in-process travel, and expected unattended hours.
Conclusion
Horizontal five-axis machining is most convincing when it solves more than one problem at once. Chip evacuation alone may not justify the layout, and multi-axis access is also available on vertical machines. But when heavy chip generation, multi-face access, setup consolidation, and pallet-based automation matter to the same part family, the horizontal architecture can become a logical process choice rather than a premium feature.
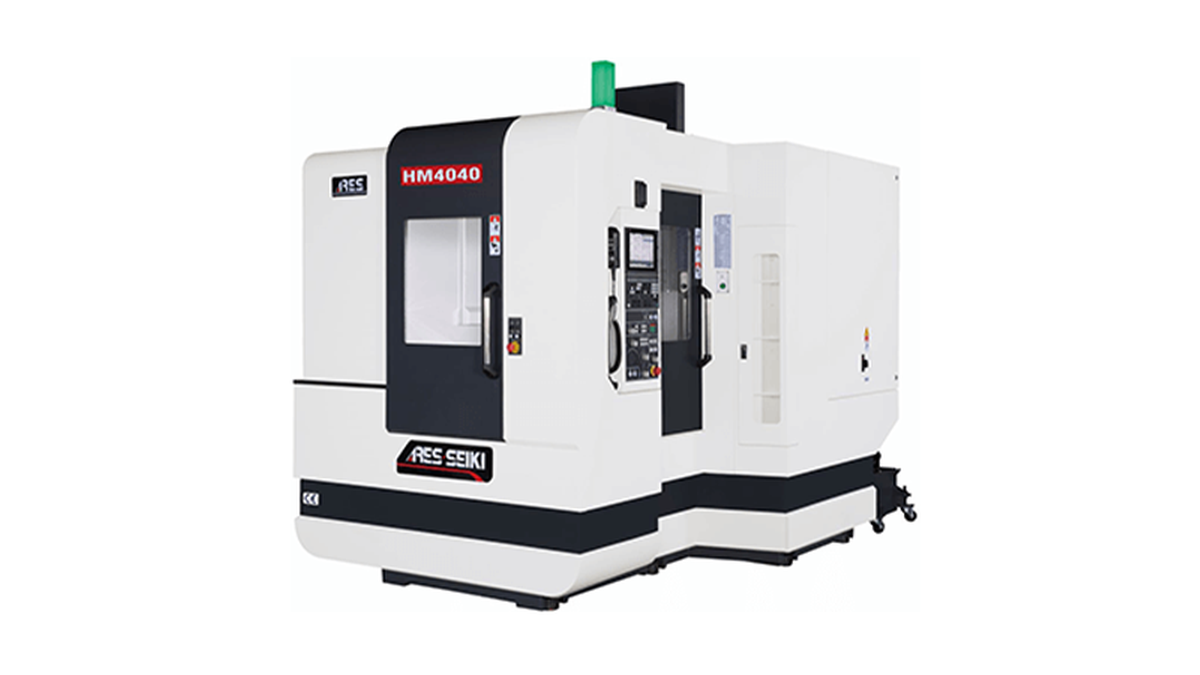
For manufacturers comparing compact horizontal five-axis platforms, the Ares Seiki HM4040 product page provides published information on spindle options, travels, table size, tool capacity, coolant flow, and chip-handling features. Reviewing those specifications alongside your part envelope, fixture plan, and automation goals can help determine whether this machine class fits the application.
Explore the HM4040 and its published specifications:
Ares Seiki – HM4040 5-Axis HMC Machine