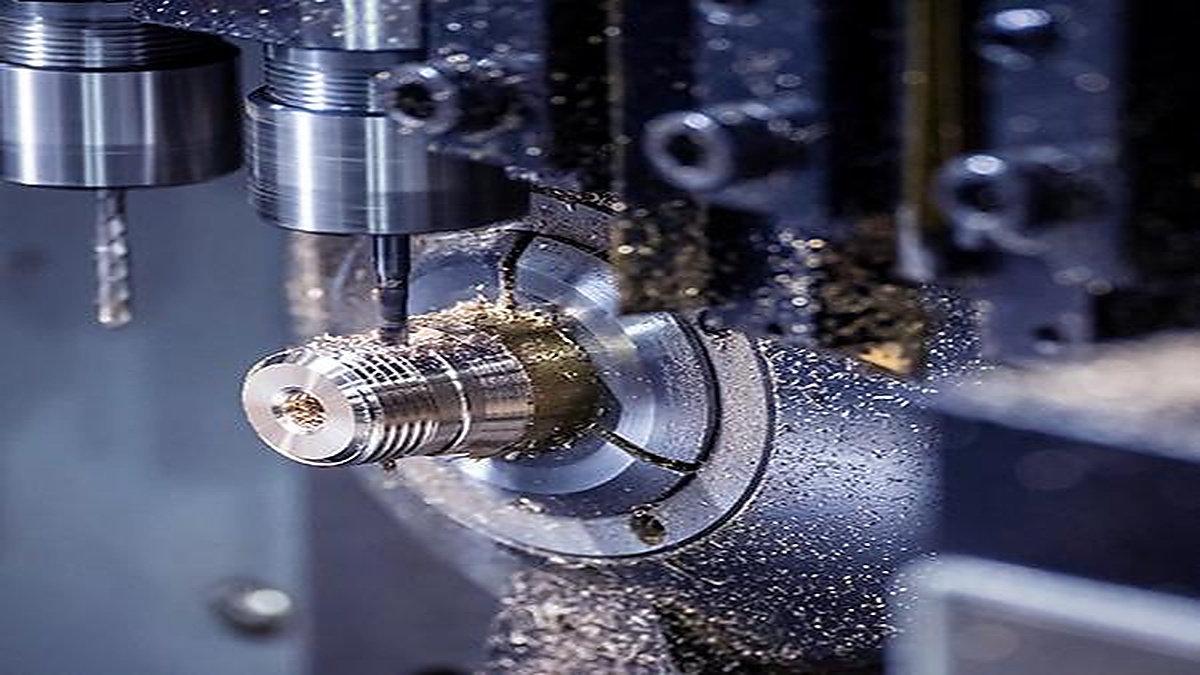
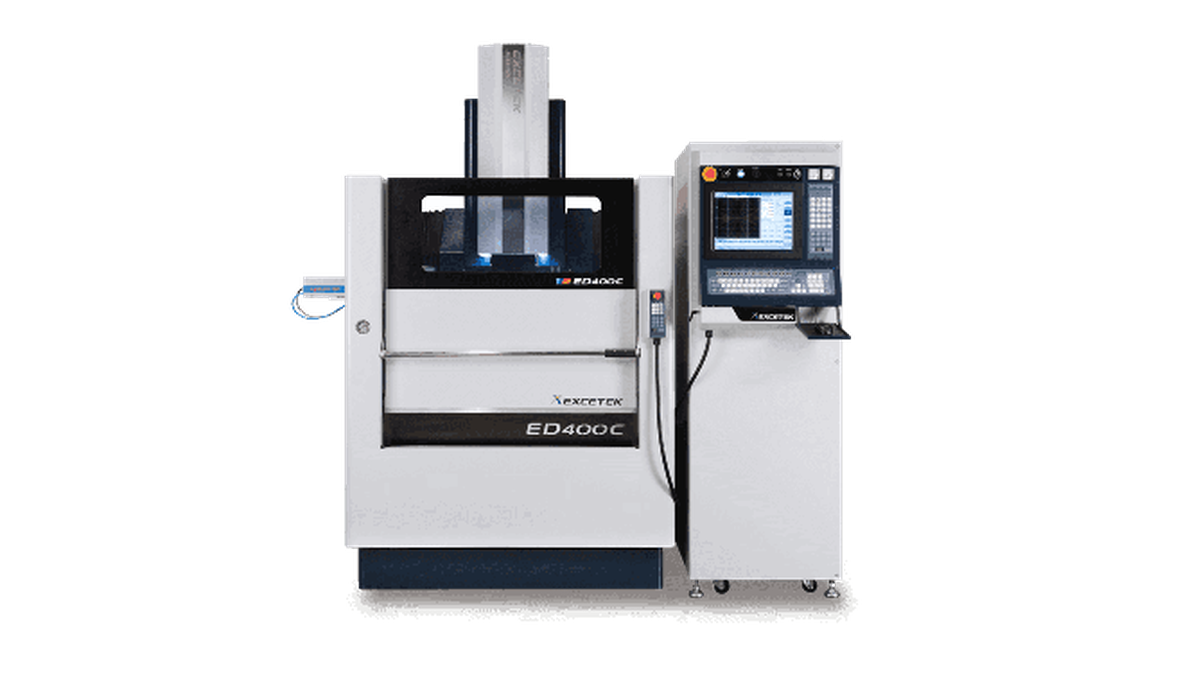
To maintain the accuracy of finished products in the manufacturing industry, rapid detection and adjustment of machine tool performance is essential.
Definition of precision:
Generally speaking, accuracy refers to the ability of the machine tool to position the tool's nose point to the programmed target point. However, there are many ways to measure this positioning capability, and more importantly, different countries have different regulations.
- Japanese machine tool manufacturers: When calibrating "accuracy", JISB6201 JISB6336 or JISB6338 standards are usually used. JISB6201 is generally used for general-purpose machine tools and ordinary CNC machine tools, JISB6336 is generally used for machining centers, and JISB6338 is generally used for vertical machining centers.
- European machine tool manufacturers: Especially German manufacturers, generally adopt the VDI/DGQ3441 standard.
- American machine tool manufacturers: Usually use the NMTBA (National Machine Tool Builder's Assn) standard.
Error sources and precision challenges of machine tools:
The final accuracy of a machine is shown by the accumulation of all possible errors.
Nowadays, the precision machinery industry has higher and higher requirements for the accuracy of finished products. In intelligent machinery and manufacturing research technology, predicting processing quality through machine conditions is an important development topic. However, regardless of the type, specification, workload, and working accuracy of the machine tool, even for the most excellent CNC machine tool, the positioning accuracy will gradually decrease over time, resulting in errors. Therefore, to ensure consistent quality of components, reduce material waste, and achieve higher production efficiency, rapid inspection and adjustment of CNC machine tool performance is necessary.
The sources of error in tool machining performance are:
-
Error of mechanical structure:
The movement of the structure under its weight and load will cause the material to deform to different degrees, resulting in errors; the size of the structural error can be known by the finite element method analysis during design.
-
Error of transmission system:
The error of the fitting clearance between the screw, the line rail, and the slider, as well as the C1 level screw pitch should be within 5μm, and the highest level of the line rail (UP level) should have an error of less than 2μm between its two parallel surfaces. However, for high-precision machinery, the whole machine design and assembly needs to find a way to eliminate these total errors and to achieve the final high-precision requirements within ±3μm.
-
Error of feedback and control:
The controller commands the output to drive the motor and uses the optical scale to receive feedback. The best existing optical scale guarantees that the error can be maintained within 3μm, but this error is determined by the accuracy of the optical scale. As long as there is no problem with the optical scale assembly, the error is fixed and can be eliminated by the error compensation of the controller.
-
Assembly error:
The straightness, perpendicularity, parallelism, flatness of the machine, and the total error of each part and moving component are generally maintained within 5μm, which is a good error range.
-
Error of temperature:
Every time the temperature rises by 1°C, it will affect the amount of deformation of iron by 11.7μm /m. During the processing, local thermal deformation occurs due to the conversion of energy, resulting in thermal deformation of the tool or workpiece, requiring compensation by the machine tool. Even with the thermal compensation function, it is only a large-scale compensation, and cannot be used for small-area compensation. The best method for high-precision machining is to control the temperature rise of the machining so that the change is less than 0.5 °C so that the accuracy can be maintained.
-
Deformation of materials:
After the material is cast, there will be extensive internal deformation, and if the material is not tempered its deformation can be large. Material conditioning is required.
-
Fixture and human operation error:
Whether the fixture is symmetrical during processing, whether the clamping force is uniform, and whether there is vibration in the environment or other interference factors will affect the processing accuracy.
-
Other errors (such as measurement or environmental factors):
In the design of the whole machine, it is necessary to consider that the total median error value should be offset by differences of positive and negative errors. Errors can be reduced by compensation, thus improving the overall accuracy of the machine. The real difficulty is that these errors vary, that is, the distribution range of their standard deviations is too large to be controlled. With dozens of error sources, to maintain a total error variation of ±3μm, the variation of each error needs to be controlled within 1μm. Maintaining the overall machine accuracy by controlling these many error sources is the difficult challenge.
Therefore, Taiwan's machine tool industry must continually improve as a whole. To beat competition, machine production factories as well as component and machining suppliers and partners must work together to improve manufacturing accuracy.