Bolt is one of the basic hardware components in the engineering and construction industry. The production process of bolts has evolved into an advanced and high-tech multi-step process.
What Is a Blot?
A bolt is a type of threaded fastener. It comes with an external male thread that is required a matching pre-formed female thread, such as a nut. Bolts are very similar to screws.
How Do Nuts and Bolts Work?
Due to the rapid industrialization and the introduction of capital-intensive technologies, nuts and bolts are widely used in the manufacturing industry as industrial fasteners to connect various machines and structures and are installed in various types of machinery and equipment.
Nuts are used as fasteners and consist of threaded holes and are used with matching bolts to fasten multiple parts together. Although the bolt is described as a threaded fastener, it consists of an external thread that requires an internal thread like a nut. Nuts and bolts complement each other. Nuts and bolts have different uses, and nuts and bolts are used to make finished products, make furniture, and are essential for making final products that can be used for consumption.
The metal fastening products produced by operators in the screw, nut, and bolt manufacturing industry can be divided into precision fastening products, customized for specific projects or customers, general fasteners, composed of screws, nuts, bolts, rivets, and washers according to the industry standard manufacturing and designed for the wider market.
Bolt Production Process
Bolts can have many different sizes and shapes, corresponding to different specifications, but the production process is roughly the same. First, the steel wire is cold-forged into the correct shape, then heat-treated to increase strength and surface treatment to improve durability, and then packaged and shipped. However, for more precise and complex bolt designs, other process steps will be added to the production process. Depending on where the fastener is used, there are many different processes matching options to produce the correct bolt.
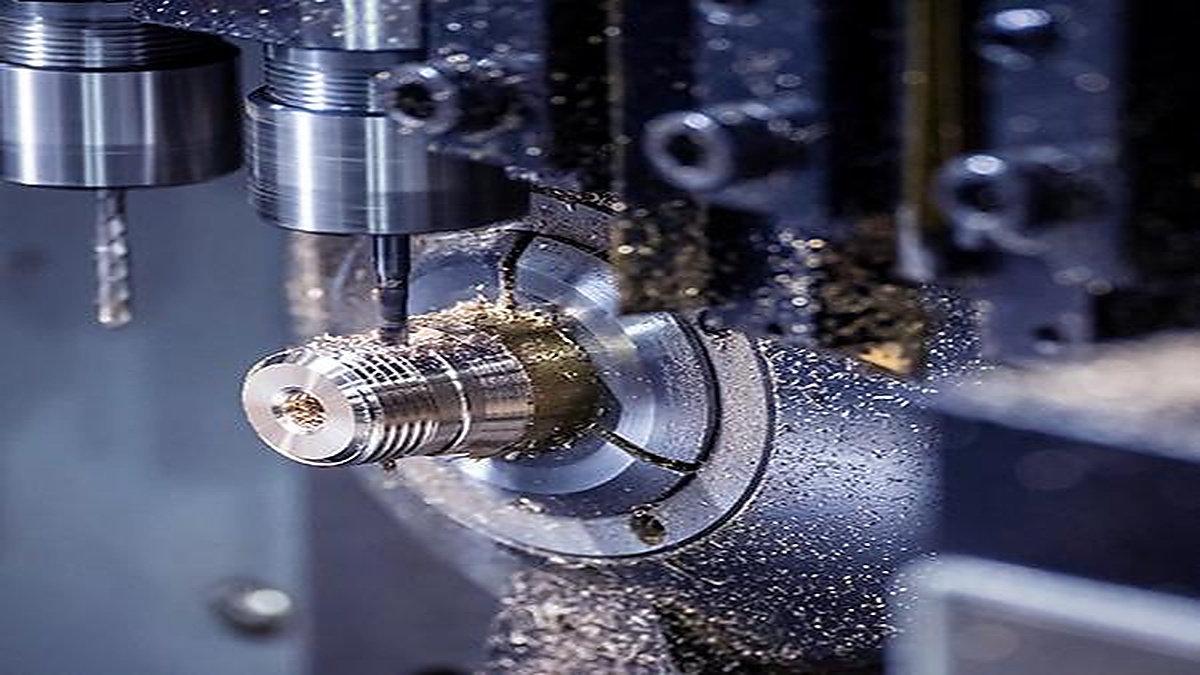
- The manufacture of bolts starts from cold forging. First, the large steel wire is uncoiled and cut into the specified length, which meets the requirements of the international ISO 898-1. Special tools are used to make the cold-forged wire rod into the correct shape. In the main process, the steel is formed at room temperature and made into a series of molds through high pressure. The tolerance requirement may be only one-hundredth of a millimeter. The precision meets its requirements. The cold forging process ensures that bolts can be produced quickly, in large batches, and with high uniformity. For more complex bolt designs that cannot be formed by cold forging alone, additional turning or drilling process assistance may be required. Turning involves rotating bolts at high speed while cutting steel to obtain the desired shape and design. Drilling can be used to drill holes in bolts. At this stage of the process, some bolts may also have washers attached.
- Heat treatment is the standard process for all bolts, including exposing the bolt to extreme temperatures to harden the steel. Thread processing is usually carried out before heat treatment and is carried out by rolling or cutting when the steel is soft. Rolling works very similar to cold forging and involves passing bolts through a die to form and mold steel into threads. Cutting involves cutting and removing steel to form threads. Since heat treatment changes the characteristics of steel to make it harder, pre-threading is easier and more cost-effective. However, the thread after heat treatment will mean better fatigue performance. For long bolts whose length exceeds ten times the bolt diameter, heat treatment can restore the steel to the original round shape of the steel wire. Therefore, it is often necessary to apply a straightening process.
- The choice of surface treatment depends on the application of bolts and customer requirements. Generally, the main concern of fasteners is corrosion resistance, so galvanized coatings applied by electrolytic treatment are a common solution. This is a process of immersing the bolt in a zinc-containing liquid and applying an electric current to cause the zinc to form a coating on the bolt. However, electrolytic treatment does increase the risk of hydrogen embrittlement. Another option is zinc flake, which has higher corrosion resistance.
The above processes are the steps in manufacturing a bolt, and the continuation is the quality control to ensure the quality of each bolt is tested and to ensure each bolt product shipped and packaged in good quality.

.jpg)
.jpg)