Spot welding is a type of welding used to weld sheets of metal together by clamping the sheets together at a single point and passing an electric current through the point to melt the sheets together.
What is the spot-welding process?
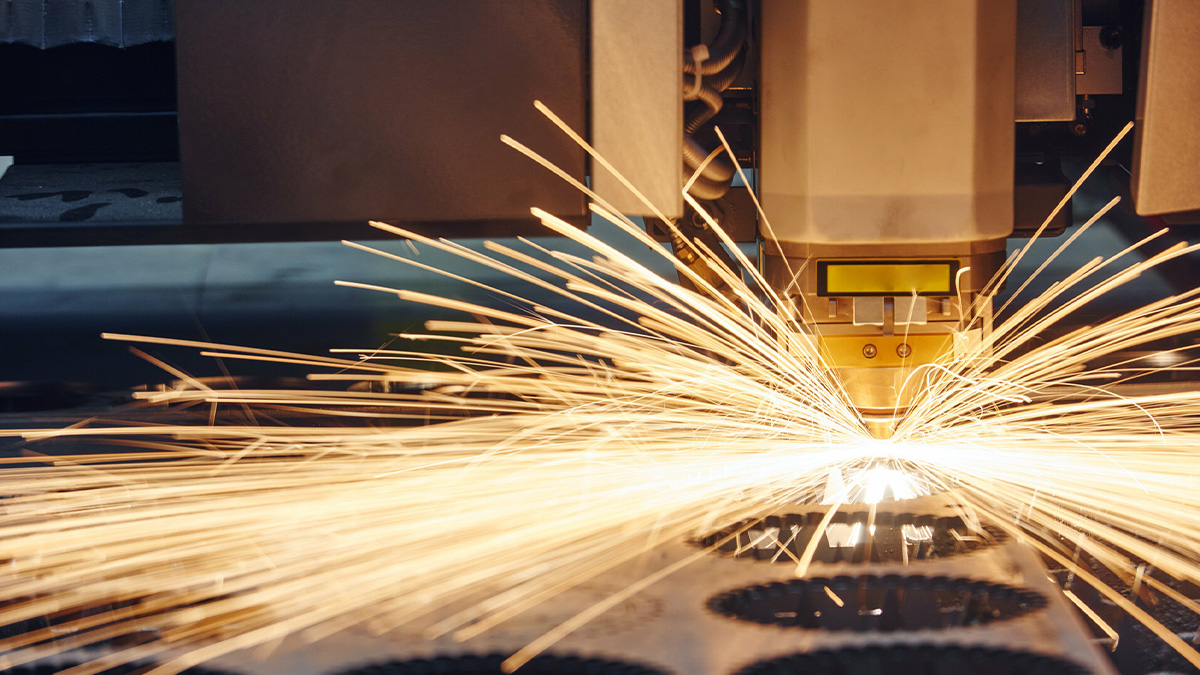
The spot-welding machine uses two electrodes to press the workpiece so that the two layers of metal form a contact resistance under the pressure of the two electrodes. As electricity flows through the workpiece, from one electrode to the other electrode, a large amount of resistive heat is generated at the contact point of the plates, and the metal in the hottest area in the center is quickly heated to a highly plastic or molten state. While continuing to maintain pressure on the contact area, the current was disconnected. As the metal cools, a thermal fusion joint is formed.
Resistance spot welding has the characteristics of low energy consumption, low cost, high quality, high efficiency, easy automation, and convenient use. No consumables, no welding rods, wires, or fluxes are required. The welding process consumes less heat, no harmful substances such as smoke and dust are created, there is no dazzling light pollution, and the working voltage is low. It is a safe, economical, efficient, reliable, and pollution-free welding method.
Spot welding is mostly used for the connection of thin plates, such as aircraft skins, aero-engine smokestacks, car cab shells, etc.
Working principle of spot-welding machine
Spot welding is mostly used for the connection of thin plates, such as aircraft skins, aero-engine smokestacks, car cab shells, etc.
The structure of the spot-welding machine is simple, it is a high-power transformer that converts a higher voltage electricity source, such as 220V AC, into a low-voltage, high-current power supply. This can be either DC or AC. This higher current, along with the resistance of the workpiece, will create the heat that will melt the weld joint.
When the current starts to flow through the electrodes, the voltage will drop. The welding machine will then regulate the working voltage during the welding process. The welding current and voltage on the welding machine can be adjusted to meet the required current for various materials being welded. Many welding machines have a cooling system that circulates water through the transformer, electrodes, and other parts to avoid heat generation.
The quality of the electrodes directly affects the welding process, welding quality, and productivity. Electrode materials commonly used are red copper, cadmium bronze, chrome bronze, etc.
The phases of the welding cycle:
- Pre-compression stage: The workpiece is placed between the two electrodes and the electrodes are pressed together, clamping the workpiece in place.
- Welding time: The welding current passes through the workpiece and generates heat to form a spot of molten metal.
- Maintenance time: The welding current is turned off and pressure is maintained on the joint until the molten metal solidifies to sufficient strength.
- Rest time: The electrode is released from the workpiece and the welding machine is allowed to cool for a brief period until the next welding cycle begins.
How to use the spot-welding machine?
- Before welding, the position of the electrode rod should be adjusted so that when the electrode is pressed to the workpiece, the electrode arms are parallel to each other.
- When welding, first clean the surface of the weldment. All dirt, oil, oxide scale, and rust must be removed before welding steel weldments to make a good contact.
- Current adjustment can be selected according to the thickness and material of the workpiece. The spring pressure nut on the electrodes can be adjusted to obtain the preferred degree of compression.
- If the welding machine has a cooling system, turn on the cooling water first and then turn on the power to prepare for welding. After the power is turned on, the power indicator light should be on.
- Place the sheets to be welded between the two electrodes and perform the spot weld. Some welding machines will have automatic controls and others may have manual controls such as a foot pedal which can be pressed to bring the electrodes into contact with the weldment and compress the workpiece.
Conditions to pay attention to when welding:
- For hot-rolled steel, it is best to sandblast or use a grinding wheel to remove the oxide scale. The workpiece can also be pickled with acid to remove metal oxides. Although uncleaned weldments can be spot welded, they can seriously reduce the service life of the electrode and reduce the production efficiency and quality of the weld.
- For hot-rolled steel, it is best to sandblast or use a grinding wheel to remove the oxide scale. The workpiece can also be pickled with acid to remove metal oxides. Although uncleaned weldments can be spot welded, they can seriously reduce the service life of the electrode and reduce the production efficiency and quality of the weld.
- Welding time: When welding medium and low carbon steel, the welding machine can use either a strong or weak weld setting. A strong setting can be used in mass production to improve production efficiency, reduce power consumption and reduce workpiece deformation.
- The shapes of electrodes vary, and are chosen according to the shape of the weldment. When installing the electrodes, pay attention to keeping the upper and lower electrode surfaces parallel. The electrode planes should be kept clean and trimmed with an emery cloth or a file.
What are the classifications of spot-welding machines?
Spot welders can be classified according to the following characteristics:
- Purpose: There are universal types and special types.
- Conduction: There are unilateral and double-sided welders.
- Transmission mode of the pressurizing mechanism: There are pedal types, motor-cam types, pneumatic types, hydraulic types, and compound types.
- According to the characteristics of operation, there are non-automation and automation.
- Characteristics of operation: There are non-automated and automated.
- Installation method; There are fixed types, mobile types, or portable types (suspension types).
- Moving direction of the electrode: There are vertical stroke (the electrode moves in a straight line) and arc stroke electrodes.
- Electric current: There are AC and DC welding machines, pulse welding machines, energy storage welding machines, and variable frequency welding machines.
Resistance spot welding machine applications:Because resistance spot welding machines have high production efficiency, low cost, good material saving, and easy automation, they are often used for small precision welding, aviation, aerospace, energy, electronics, automotive, light industry, and other fields.
Capacitive spot welder:A capacitive spot-welding machine (also known as capacitive energy storage spot welding machine) passes alternating current through a rectifier to convert it to DC, and then goes to a capacitor to charge the capacitor. The electricity is then released as a pulse through the contact points of the workpiece to weld the metal.
What are the characteristics of a capacitive spot-welding machine?
- Energy saving and high output efficiency.
- The power taken from the grid is low, so the impact on the grid is small.
- The output voltage is stable.
- The welding is firm, and the solder joints are not discolored.
- Saves the grinding process and has high efficiency.
Capacitive spot-welding machine related products:
- Microcomputer chip operation control, the error of charging and discharging current setting value is maintained at less than 2%.
- Most DC spot welding machines adopt an LED display to set the power, so charging and discharging electric power changes can observed.
- Japanese-made high-efficiency rapid charge and discharge capacitors have a long service life, with stable and accurate current output.
- The maximum voltage of the operating end of the spot-welding machine is 12 VDC. Low voltage means high welding safety.
- The discharge speed is only 10 microseconds, and the heating rate is high. A capacitive spot-welding machine can easily spot-weld aluminum, copper, gold, silver, and other high thermal conductivity materials. The charging time is 0.25 seconds, so each cycle only takes about 0.26 seconds.
- DC SPOT current output is accurate, making high quality, firm, clean solder joints with no browning or discoloration.
- Precision capacitive spot-welding machines developed with high-quality parts from Europe, America and Japan can provide high efficiency spot welding with low failure rate. They are not only used for non-ferrous metals such as gold, silver, and tin-plated soldering parts, but also for precise welding of ferrous metals such as iron and stainless steel. They have the advantages of being efficient, accurate, energy-saving, and material saving. They have fast welding speeds and stable welding quality and can eliminate the need for technical personnel to operate them.