Deburring is the removal thorns or burrs that have formed around the machined edges of a workpiece. The burr may seem small, but it can directly affect the quality and precision of the product.
The Prevalence and Danger of Glitches
Burrs are an inevitable product of metal processing and are difficult to completely avoid. The existence of burrs not only affects the appearance of the product but also affects the assembly and performance of the product, accelerates the wear between the equipment, and reduces the service life. With the development of high technology and the improvement of product performance, the requirements for product quality are becoming more and more strict, and it is more and more important to remove the burrs of mechanical parts. The existence of burrs has an impact on product quality and product assembly, use, dimensional accuracy, and shape and position accuracy.
What is a Burr?
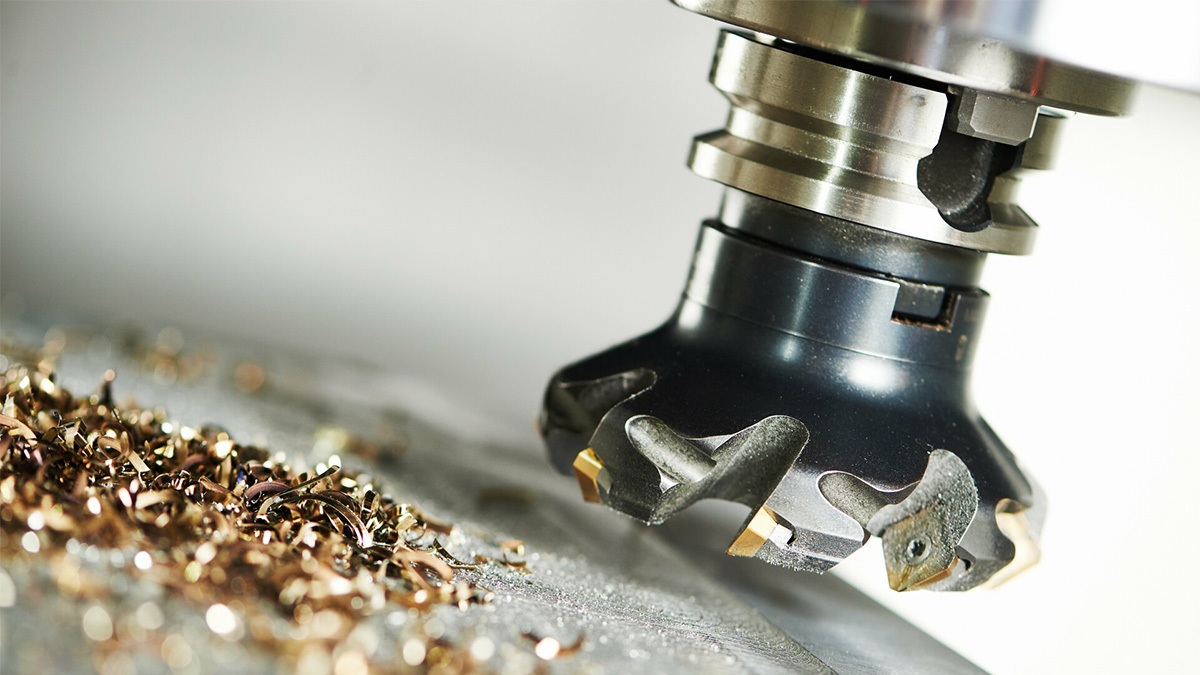
A burr refers to excess iron filings generated on the edge of a product when the workpiece is being processed. They are formed during cutting, grinding, milling, and other similar chipping processes.
What is Deburring?
During the machine processing or metal workpieces, rough edges or protrusions are often created. These raised protrusions and shavings which remain attached to the workpiece are called "burrs," and the process by which they are removed is called deburring.
Abrasives can be used to remove burrs, or the workpiece can be wiped with a sticky cloth to remove the burrs. Deburring and polishing of more than one area of the metal component may be necessary, as burrs and chips can occur on seams and edges which are not always easy to see or reach.
Deburring is important to the quality, aesthetics, functionality, and smooth operation of the working part. It is equally important for safety, because even small notches can cause moving parts to catch, creating potential accidents, injuries, or unnecessary production delays.
What are the Methods of Deburring?
Chemical removal and physical removal.
-
Electrolytic deburring:
Electrical energy can be used to dissolve and remove burrs. The part to be de-burred is connected to the positive pole (anode) of a DC power supply and immersed in an electrolyte solution creating an electrode in the solution. Another electrode is connected to the negative pole (cathode) of the DC power supply and placed into the solution, maintaining a gap between the two poles to allow the electrolyte to circulate. When the anode and the cathode are and supplied with direct current, an electrochemical reaction occurs on the surface of the anode. The dissolved metal on the surface of the part and the electrolyte form a viscous liquid concentrated in the low recesses on the surface of the part, with high resistance and corrosion. The edge of the burr protruding furthest from the surface of the part will dissolve at the fastest rate and will continue to dissolve until all the burrs are dissolved. The edges of the part will gradually form rounded corners as the part is deburred.
This method is suitable for both non-ferrous and ferrous metal parts, and especially for parts with complex shapes and inner holes, cross holes, and burrs on inner surfaces that are difficult to remove by mechanical and manual methods.
-
Chemical deburring:
This process is similar electrolytic deburring but instead of electricity removing the burrs, a chemical reaction occurs on the surface of the part to be deburred, dissolving the burr. Ions gather on the surface of the workpiece and form a film with high resistance and low conductivity, which protects the surface of the workpiece from corrosion. Depending on the material of the workpiece being deburred, different chemical solutions are used. Common materials used for chemical deburring are hydrochloric acid, phosphoric acid, sulfuric acid, diphenylamine hydrochloride, and water. Chemical deburring is suitable for small metal parts and can remove fine burrs less than 0.07 mm thick.
-
High temperature deburring:
The parts to be deburred are placed in a tightly sealed chamber, and a mixture of hydrogen and oxygen are fed into the chamber under pressure. A spark is introduced to ignite the mixture. As the mixture explodes, it instantly releases a lot of heat at a temperature is as high as 3,300℃ or more. Due to the extremely short explosion time, the burrs are burned away, and other parts of the workpiece do not have enough time to be affected. During the explosion, the high-pressure gas is pervasive, and the burrs of all inner holes, cross holes, grooves, deep holes, etc. of the parts can be burned off. A special high-temperature deburring tool is required. This method of deburring is suitable for metal, plastic, and rubber parts of any structural shape, especially parts with complex shapes that have burrs in areas that are difficult to remove by hand.
-
Rolling and deburring:
The workpiece to be deburred can be placed into a drum with an abrasive material and rotated. During the rotation of the drum, abrasion occurs between the abrasive and the workpiece, removing the burrs. There are special centrifugal deburring machines that use centrifugal force to create a greater force of the adhesive onto the workpiece, making the polishing and deburring process quicker. Abrasives can be quartz sand, sawdust, alumina, ceramics, dolomite, silicon carbide, metal rings, etc. They can be chosen according to the material, shape, and size of the part, as well as the location and size of the burr. With this method, the deformation of the parts is small, the equipment is simple, the operation is easy, and the sources of abrasives are wide. One drawback is that large burrs are difficult to remove.
-
Floating deburring spindle for deburring:
Deburring can be done on a CNC machine as an added final machine processing step. A floating deburring spindle is installed on machining center. The spindle can be automatically replaced through the quick-change interface to realize multi-process processing. It is an important step in the machining of cylinder heads, crankshafts, connecting rods, engine blocks, wheel hubs, gas turbine blades, gears etc. This method helps avoids the time-consuming process of manual grinding and deburring. It is highly automated, and greatly improves efficiency and accuracy. It saves on labor costs and reduces the defect rate of parts caused by manual operation errors. The floating mechanism function allows the deburring tool to automatically offset radially or axially according to the actual shape of the workpiece.
Applications of Deburring:
There are many unique applications for deburring. Besides the deburring of machined workpieces, deburring can be used for the edges of especially thin workpieces, such as the fine edges of small workpieces cut from sheet metal. Deburring is also used for the surface grinding of pipes, connections, and shafts. Burrs that appear in the inner hole during punching or laser processing can be removed with various deburring methods.