How spray timing, pressure transients, material viscosity and motion synchronization affect coating consistency
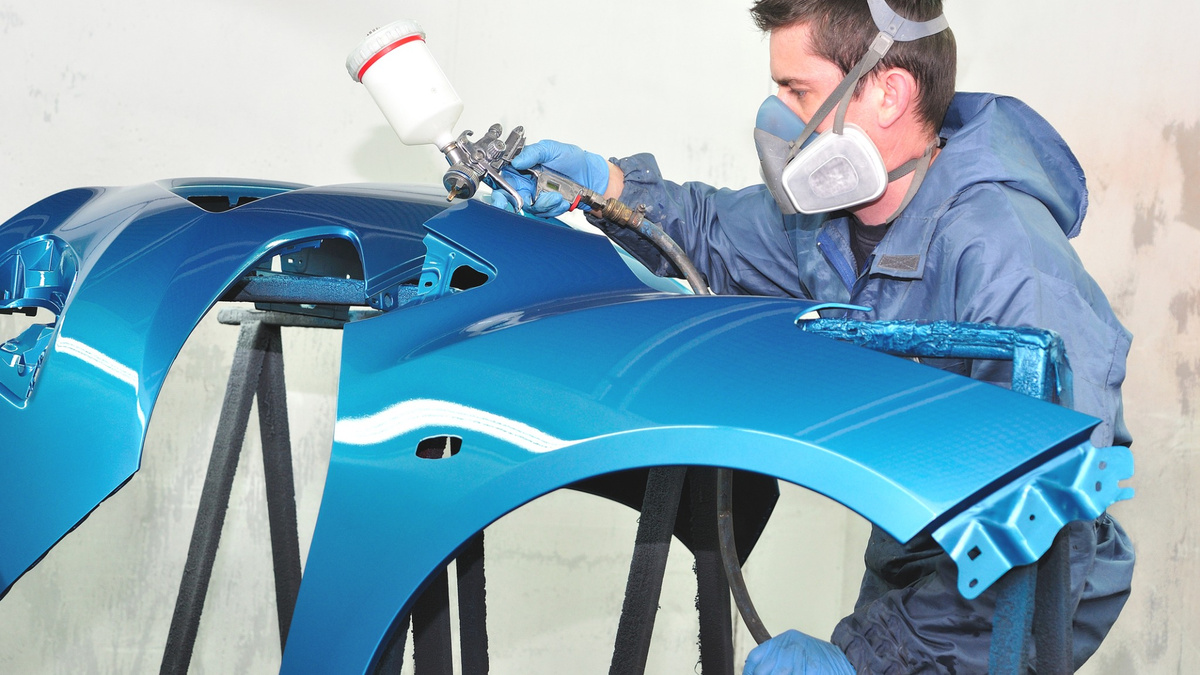
Automatic spray systems are usually tuned around steady-state conditions: stable fluid pressure, established atomizing air, constant conveyor speed, and repeatable gun-to-part position. The difficult moments are often the first and last fractions of a second. At line starts and stops, the system is entering or leaving that steady state. As a result, an otherwise well-adjusted automatic air spray gun can produce a heavy band, dry edge, spit, or thin patch near the beginning or end of a coated area.
Understanding these defects means treating the spray gun as part of a timed pneumatic, fluid, and motion-control system rather than as an isolated nozzle.
Air and Fluid Do Not Change State at the Same Instant
In an automatic air spray gun, coating flow is commonly started by a pneumatically operated needle or piston, while atomizing and pattern air may be controlled separately. Even if a PLC sends commands simultaneously, the physical response is not. Solenoid valves need switching time, air travels through tubing, and the gun piston must move.
If fluid reaches the nozzle before sufficient atomizing air is available, the first material may leave as large droplets or a short surge, creating a wet start. At shutdown, if atomizing air disappears before fluid flow fully stops, the last material can form a spit or heavy tail.
ANEST IWATA's guidance for certain high-performance automatic guns illustrates the principle: atomizing and pattern air are switched on about 0.2 seconds before piston operation at spray start and switched off about 0.2 seconds after piston operation at spray stop. Exact delays vary by equipment, but the general objective is to establish atomization before fluid delivery and maintain it briefly while fluid flow ends.
Fluid Pressure Can Surge or Dip During Triggering
Pressure measured during continuous spraying may look correct while pressure at the gun behaves differently during opening and closing. When the fluid needle opens, a hose, regulator, pump, or pressure pot may release stored pressure, briefly increasing flow. The opposite can also occur: a restrictive supply line or undersized regulator may let pressure fall when demand suddenly rises, producing a thin start until the system recovers.
The effect can be stronger when several guns trigger together. Pump pulsation, long flexible hoses, regulator response, and regulator-to-gun distance can all influence the transient. For diagnosis, observe pressure as close to the gun as practical during the trigger event, not only during steady spraying.
Pneumatic hardware also matters. Automatic-gun documentation notes that undersized solenoid passages and excessive hose length can delay gun operation, demonstrating why the control circuit itself should be considered when start and stop response is inconsistent.
Viscosity and Temperature Change Spray Response
A correctly timed system can still become inconsistent if coating viscosity changes. Temperature is a common reason. Warmer coating generally flows more easily, while cooler material resists flow and may atomize differently.
Graco's spray-technology guidance explains that viscosity, pressure, fluid-tip selection, and atomization are closely related. Sames technical literature likewise documents how temperature-driven viscosity changes can significantly alter coating flow and finish behavior.
This is especially relevant at morning start-up, when coating, hoses, pumps, and the booth may be cooler than later in the shift. Settings that work after an hour of production may therefore behave differently on the first parts.
Motion Timing Can Look Like a Gun Problem
The spray itself may be stable while the command occurs at the wrong position relative to the part. On a conveyor or robot, a small timing error becomes a physical offset. Turning on too early can create excess build before the intended target zone; turning on too late leaves a light leading edge. The same principle applies at the trailing edge.
Sensor placement, PLC scan time, solenoid response, conveyor acceleration, encoder calibration, and robot path timing all contribute. If the defect appears only at part entry or exit, changing spray pressure is often less useful than checking synchronization first.
This distinction is important because steady-state spray quality and positional coating accuracy are separate issues. A gun can produce a uniform fan while still being commanded at the wrong moment.
Gun Condition Still Matters
Transient defects should not distract from basic gun maintenance. Graco's troubleshooting guidance identifies dirty or plugged air-cap holes, worn or plugged tips, excessive atomization air, incorrect fluid flow, and excessive gun distance as causes of uneven patterns, dry spray, runs, or rough finish.
A marginal air cap may look acceptable in the center of a pass yet become more obvious during the weaker transient spray cloud at start-up or shutdown.
| Observed defect |
First area to investigate |
| Heavy start |
Fluid before atomizing air; pressure surge |
| Thin or dry leading edge |
Fluid lag, pressure dip, or late trigger |
| Spit or heavy tail |
Air ending before fluid fully closes |
| Defect shifts with line speed |
Sensor, PLC, encoder, or motion timing |
| Defect varies by shift |
Coating temperature and viscosity |
| Uneven fan through the whole pass |
Air cap, tip, contamination, or alignment |
A Practical Troubleshooting Sequence
Start by confirming whether the defect occurs at a repeatable time or position. Then verify the actual air-on, fluid-on, fluid-off, and air-off sequence. Check solenoid capacity and pneumatic hose length, because restrictive valves or long lines can delay operation.
Next, watch fluid pressure during triggering and check whether multiple guns share a supply problem. Confirm coating temperature and viscosity under real production conditions, especially at cold start. Finally, inspect the air cap, nozzle, needle, seals, and gun-to-part geometry.
Make one change at a time and validate film build across several consecutive parts. The goal is not one visually improved sample but a repeatable transition from off to stable spray and back to off.
FAQ
1. Why is the first part after line start often heavier?
Static pressure may be stored in the fluid system, or atomizing air may not be fully established when coating begins to flow. Cold, more viscous material can also change the response.
2. Should atomizing air turn on before the paint?
Often, yes. A short air lead can reduce the chance of large initial droplets. The correct delay depends on the gun, valves, hose layout, coating, and controller rather than on one universal setting.
3. Can more atomizing pressure fix a heavy start?
Not necessarily. Additional air will not correct a fluid-pressure surge or poor trigger sequence, and excessive atomizing air can contribute to overspray or dry spray.
4. Why is coating thin only at the leading edge?
Typical causes include delayed fluid response, a temporary pressure dip when the gun opens, or a spray-on command that occurs too late relative to part motion.
5. Does hose length affect automatic gun response?
Yes. Long or undersized pneumatic lines can increase response delay, while fluid hose volume and elasticity can influence pressure behavior during rapid opening and closing. Equipment manufacturers therefore specify practical limits for valve capacity and pneumatic tubing in some installations.
6. How do I separate a gun problem from conveyor timing?
If the defect moves when line speed or trigger position changes, synchronization is a strong suspect. If the spray fan remains distorted during steady operation, inspect the air cap, nozzle, fluid supply, and material condition instead.
Conclusion
Uneven coating at line starts and stops is often a transient-control problem rather than a steady-state spray problem. Common contributors include mismatched air/fluid timing, pressure changes, temperature-dependent viscosity, motion-control delays, and basic gun condition.
Troubleshooting becomes faster when these factors are observed during the actual trigger transition rather than judged only from continuous spraying. Recording timing, pressure, temperature, and defect position can reveal relationships that are difficult to see through visual inspection alone.
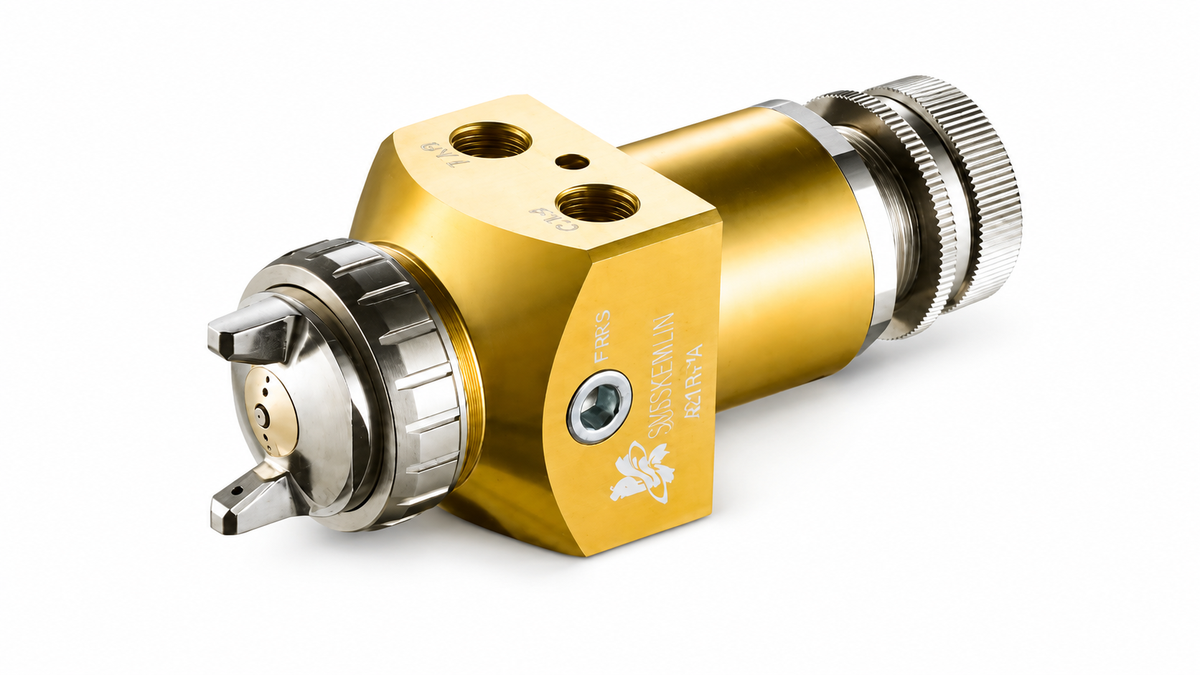
For coating-line teams evaluating automatic air spray equipment, comparing control-air arrangements, fluid adjustment options, nozzle configurations, and integration requirements can also help reduce start/stop variability at the design stage. For an overview of available configurations, you can explore Ranox automatic air spray gun options.